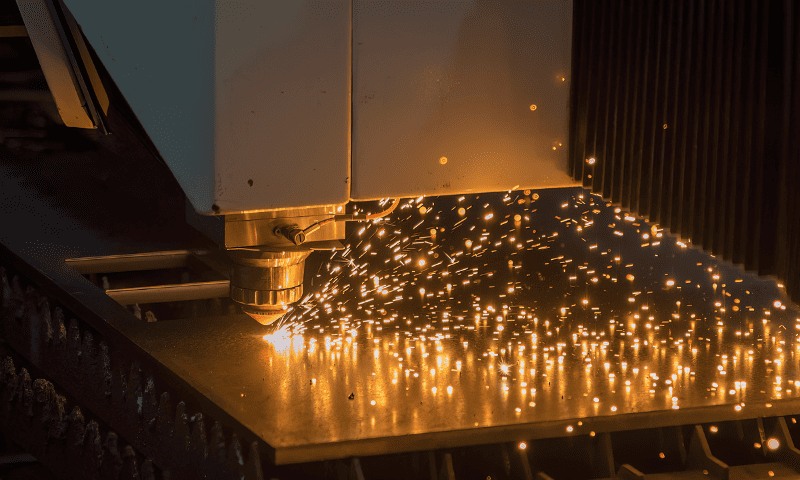
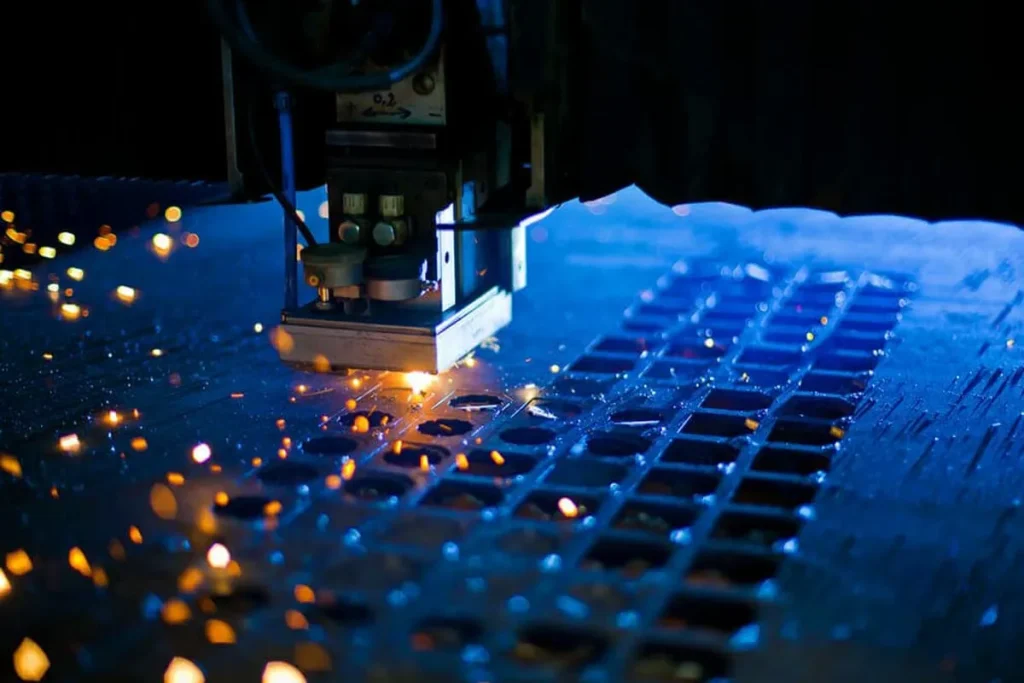
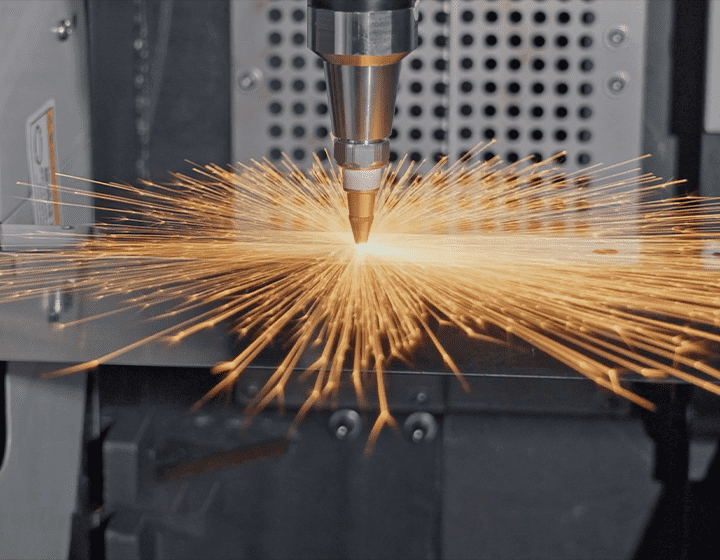
Laser cutting is a sophisticated thermal cutting process that utilizes a focused, high-power-density laser beam to rapidly melt, vaporize, or reach the ignition point of materials. Simultaneously, a high-speed coaxial airflow (assist gas) removes the molten matter, achieving a precise cut. Fiber laser technology is widely applied in processing stainless steel, carbon steel, aluminum alloys, and brass due to its non-contact nature, high speed, and smooth kerf quality.
Key parameters affecting cut quality include cutting speed, laser power, assist gas pressure/purity, focal position, nozzle characteristics, and material properties.
Part 1: Stainless Steel Laser Cutting (Fusion Cutting)
Laser cutting of stainless steel primarily utilizes the Fusion Cutting principle. The laser melts the metal, and a non-oxidizing assist gas (typically Nitrogen, Argon, or Helium) blows away the slag. Since no exothermic oxidation reaction occurs, this process requires significantly less energy than vaporization cutting but relies heavily on gas dynamics for a clean finish.
5 Common Defects in Stainless Steel Cutting
Defect Type
Possible Causes
Solutions
Dross at the
Bottom (Slag)
• Focal position too low • Feed rate too high • Laser power too low
• Raise the focal position • Decrease the feed rate • Increase the laser power
Rough Cutting
Edge
• Nozzle misalignment • Focal position too high • Assist gas pressure too low • Cutting speed too low • Nozzle orifice obstruction
• Re-align the nozzle • Lower the focal position • Increase assist gas pressure • Increase cutting speed • Inspect or replace the nozzle
Edge Burning /
Overheating
• Feed rate too low • Focal position too high • Assist gas pressure too low • High material temperature (heat accumulation)
• Increase the feed rate • Lower the focal position • Increase assist gas pressure • Cool the material / allow cooling time
Incomplete
Penetration
• Power too low • Feed rate too high • Assist gas pressure too high
• Stop immediately to prevent back-splatter on optics • Increase laser power • Decrease feed rate • Decrease assist gas pressure
Oxidation (Yellow/
Black Edges)
• Insufficient Nitrogen purity • Oxygen or air present in the gas lines
• Verify Nitrogen purity (≥ 99.95% recommended) • Increase delay for gas line purging • Check gas lines for leaks/sealing issues
Summary (Stainless Steel): The principles for cutting aluminum and brass are identical to stainless steel. Due to their high reflectivity, these materials require a lower feed rate compared to stainless steel of the same thickness. Troubleshooting for these non-ferrous metals should follow the stainless steel guidelines provided above.
Part 2: Carbon Steel Laser Cutting (Flame Cutting)
Laser cutting of carbon steel utilizes Oxygen Cutting (Flame Cutting). The laser acts as a preheating source, while Oxygen reacts chemically with the metal. This exothermic reaction releases significant heat, assisting the laser in melting the material and blowing out the molten oxides. This process allows for much higher speeds when processing thick plates compared to fusion cutting.
6 Common Defects in Carbon Steel Cutting
Defect Type
Possible Causes
Solutions
Incomplete Cut
at the Bottom
• Feed rate too high • Laser power too low • Assist gas pressure too low • Focal position too high
• Decrease the feed rate • Increase the laser power • Increase assist gas pressure • Lower the focal position
Excessive Slag
Attachment
• Feed rate too high • Assist gas pressure too low • Focal position too high
• Decrease the feed rate • Increase assist gas pressure • Lower the focal position
Rough or
Corrugated
Surface
• Feed rate too high • Inadequate assist gas pressure • Low gas purity • Focal position too high
• Decrease the feed rate • Increase assist gas pressure • Use higher purity Oxygen • Lower the focal position
• Re-center the nozzle with the beam path • Replace the nozzle
Over-burning
of Edges
• Assist gas pressure too high • Damaged nozzle • Nozzle diameter too large • Low-quality material (internal defects)
• Decrease assist gas pressure • Replace the nozzle • Install a properly sized nozzle • Use high-quality, uniform steel plates
Burnt Corners
or Rounding
• Focal position too high • Assist gas pressure too high • Feed rate too low • Material overheating
• Lower the focal position • Decrease assist gas pressure • Increase the feed rate • Cool the material between cuts
Summary (Carbon Steel): The cutting principles for structural steel and manganese steel are identical to carbon steel. Therefore, the process tuning and troubleshooting strategies for these alloys can be cross-referenced with the carbon steel methods outlined above. Mastering these 6 core strategies will resolve the vast majority of carbon steel fabrication issues.