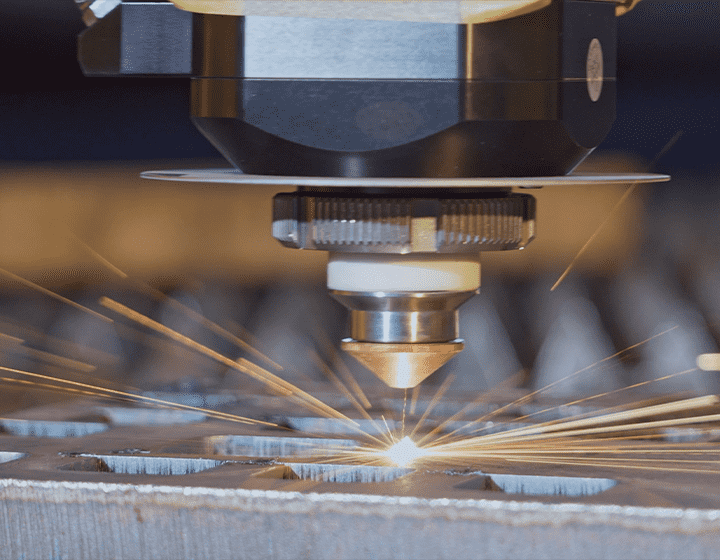
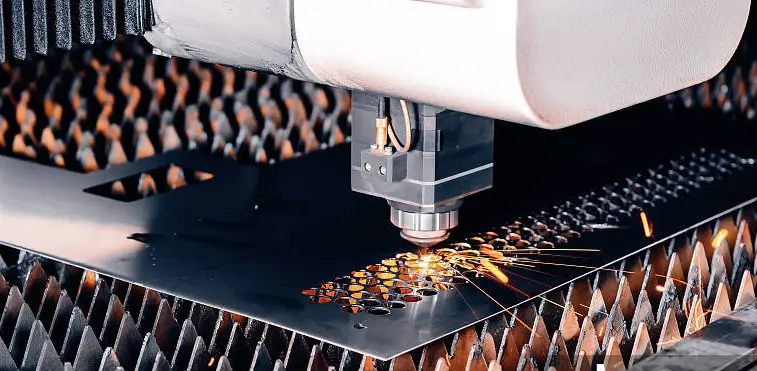
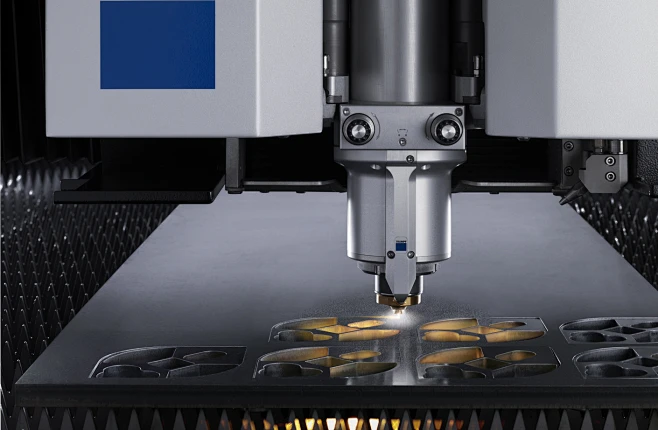
Laser cutting was first applied to industrial manufacturing in the 1970s. The process begins when a focused laser beam irradiates the workpiece surface, causing the temperature in the targeted area to rise sharply until the material melts or vaporizes. Once the beam penetrates the workpiece, the cutting process follows a pre-programmed contour, continuously melting and separating the material. This high-precision thermal separation process is what we define as Laser Cutting.
PART 1:The six core components of laser cutting parameters
1. Laser Power
Laser power is the most vital parameter of any fiber laser cutter. Higher power allows for faster cutting speeds and greater material thickness capacity.
Material Reflectivity:
For highly reflective materials, a significant portion of energy is reflected rather than absorbed. Therefore, higher laser power is required to maintain sufficient energy for the cut.
Thermal Conductivity:
Materials with high thermal conductivity dissipate heat quickly throughout the workpiece. Increasing laser power is necessary to keep the cutting zone at its melting or boiling point.
High Melting Point:
Materials with high melting points require increased power density to achieve rapid phase transformation.
2. Cutting Speed
For a given power level, as material thickness increases, the beam must penetrate deeper, which naturally limits the speed.
Surface Roughness:
Research indicates a U-shaped relationship between cutting speed and edge roughness. There is an optimal speed point where the cut surface achieves its minimum roughness (maximum smoothness).
Efficiency vs. Power:
Generally, faster speeds require higher power. The optimal speed is determined by the material type, thickness, hardness, laser power, and spot diameter.
3. Cutting Thickness Capacity
The maximum thickness a machine can cut is influenced by:
Equipment Power:
Higher wattage typically equates to higher thickness capacity.
Material Properties:
Hardness, density, and toughness dictate how easily the laser penetrates.
Cutting Technology:
Different methods (Laser, Waterjet, Plasma) have varying thickness thresholds.
4. Assist Gas and Flow Rate
During fusion cutting, the laser melts the material while the assist gas (Nitrogen, Oxygen, or Air) blows the liquid metal away.
Gas Pressure:
The pressure must be sufficient to clear the kerf of molten slag effectively.
Nozzle Geometry:
The shape of the nozzle affects gas distribution and flow characteristics, requiring precise synchronization with the flow rate for optimal results.
5. Beam Quality and Focal Position
The laser’s beam mode is critical. In non-oxygen-assisted cutting, the kerf width is nearly equal to the focal spot diameter.
Focal Length:
A shorter focal length lens produces a smaller spot but has a shorter depth of focus, requiring tighter control of the nozzle-to-workpiece distance.
Defocus Amount (Focal Position):
Typically, a negative defocus (where the focal point is placed below the material surface) is selected to optimize cutting speed and depth.
6. Nozzle Characteristics
The nozzle ensures that the gas flow and the optical axis remain coaxial. The exit diameter must be selected based on material thickness. Maintaining a constant distance between the nozzle and the workpiece is essential for process stability.
Part 2: Strategies for Improving Laser Cutting Performance
To enhance efficiency, improve cut quality, and reduce operational costs, the following optimization strategies should be implemented:
High-Power Integration:
Upgrading to higher power laser sources significantly boosts speeds and reduces theHeat-Affected Zone (HAZ)and material deformation.
Parameter Fine-Tuning:
Systematically adjust power, speed, gas pressure, and nozzle distance based on specific material trials to find the “sweet spot” for every job.
Automatic Focusing Systems:
Implement auto-focus heads that adapt to different material thicknesses and types in real-time to ensure consistent precision.
Minimizing Non-Cutting Time:
Optimize rapid traverse speeds to ensure the cutting head moves efficiently between paths.
Edge Detection & Alignment:
Use automatic sensing to detect material edges and tilt angles, reducing setup time and material waste.
Nesting Software Optimization:
Utilize advanced nesting algorithms to plan the most efficient cutting paths and maximize material utilization.
Routine Maintenance:
Regularly clean optical components (lenses/mirrors), calibrate the machine, and replace consumables to maintain peak performance.
Environmental Control:
Maintain a clean, temperature-controlled, and low-humidity environment to protect the laser source and sensitive electronics from dust and moisture.
Advanced Control Systems:
Adopt modern CNC systems and software that offer higher response speeds and support for complex geometries.
Conclusion: Understanding the interplay between laser cutting parameters and material properties is the foundation of high-quality fabrication. By mastering these principles and implementing proactive optimization strategies, manufacturers can achieve superior precision, faster throughput, and lower overall production costs.