News
Principles and Classifications of Laser Cutting Technology : A Comprehensive Technical Guide
Since its first industrial application in the 1970s, laser cutting has evolved into the most critical thermal cutting technology in modern manufacturing. Its versatility spans a wide range of materials, including sheet metal, plastics, glass, ceramics, semiconductors, textiles, wood, and paper, playing an indispensable role in industries such as automotive, aerospace, electronics, and light manufacturing.
1. Fundamental Process Principles
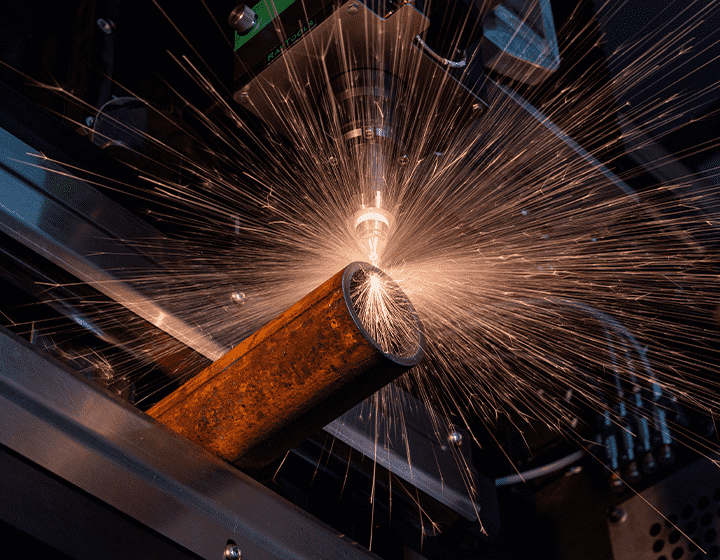
The fundamental mechanism of laser cutting technology involves directing a high-power-density focused laser beam onto the workpiece surface. The material in the irradiated zone rapidly absorbs the light energy and converts it into heat, causing the temperature to surge to its melting or boiling point almost instantaneously.
Once the laser beam penetrates the workpiece, the cutting process begins. The beam moves along a pre-programmed contour line, continuously melting the material in its path. Simultaneously, an assist gas (typically compressed air or a specific process gas) is injected into the kerf at a calculated pressure. This gas stream blows away the molten slag, creating a narrow cut with a width approximately equal to the diameter of the focused spot, thus achieving precise separation.
2. Key Cutting Classifications and Technical Features
Based on the type of assist gas used and the material removal mechanism, laser cutting is categorized into several standard process modes:
A. Flame Cutting (Oxygen Cutting)
Flame cutting is the industrial standard for processing mild steel. It uses Oxygen (O₂) as the assist gas at pressures up to 6 bar.
Mechanism:
- Once the laser heats the metal to its ignition point, the Oxygen reacts violently with the high-temperature metal (oxidation). This exothermic reaction releases significant chemical energy—up to five times the energy of the laser beam itself.
Advantage:
- This synergy of laser heating and thermochemical reaction provides high efficiency and cost-effectiveness, particularly for thick low-carbon steel plates.

B. Fusion Cutting (Inert Gas Cutting)
Fusion cutting is the most versatile process for metals and meltable non-metals like ceramics. It utilizes Nitrogen (N₂) or Argon (Ar) as the assist gas at pressures ranging from 2 to 20 bar.
Mechanism:
- As inert gases, Nitrogen and Argon do not react chemically with the molten metal. They act solely through physical force to eject the melt from the kerf.
Advantage:
- The inert gas creates a protective atmosphere around the cutting edge, preventing oxidation. This results in clean, oxide-free edges that are ideal for stainless steel and aluminum.

C. Compressed Air Cutting
For processing thin sheets, compressed air is often used directly as the cutting gas source (typically at 5-6 bar).
Mechanism:
- Since air is approximately 78% Nitrogen, the mechanism is similar to fusion cutting. However, the trace Oxygen in the air can cause minor oxidation.
Advantage:
- It offers a balance of cost-efficiency and convenience for applications where minor oxidation is permissible.
D. Plasma-Induced High-Speed Cutting
In certain fusion cutting scenarios, a plasma cloud—consisting of ionized metal vapor and assist gas—can form.
Mechanism:
- This plasma cloud absorbs energy fromCO₂ laser beams and re-radiates it to the workpiece surface, enhancing energy coupling and accelerating the melting process.
Note:
- This energy enhancement occurs only with CO₂ lasers, as the plasma cloud is transparent to solid-state lasers (such asFiber Lasers).
E. Vaporization Cutting (Sublimation Cutting)
Vaporization cutting removes material through direct sublimation, minimizing the Heat-Affected Zone (HAZ) in surrounding areas.
Continuous CO₂ Lasers:
- Ideal for materials with low vaporization heat and high absorption rates, such as plastic films, wood, paper, and foam.
Ultra-Short Pulse Lasers (Picosecond/Femtosecond):
- These have extended vaporization cutting into the metal domain. Because the pulse duration is shorter than the thermal diffusion time to the surrounding lattice, the material sublimates directly. This “Cold Processing” results in burr-free, high-precision cuts with no significant HAZ, making it perfect for micro-processing of heat-sensitive materials.

3. Critical Process Parameters and Control Strategies
The quality of laser cutting is governed by several interconnected parameters:
Polarization Degree:
- This indicates the efficiency of polarization state conversion (typically around 90%). It directly impacts edge roughness and perpendicularity.
Focal Diameter:
- This determines the kerf width. Using a focusing lens with a smaller focal length creates a narrower cut, increasing machining precision.
Focal Position:
- This determines the spot size and power density distribution on the surface, affecting the taper of the cut. Precise control is vital for maintaining consistency between the top and bottom kerf widths.
Laser Power:
- Must be strictly matched to the material type and thickness. Power must be high enough to exceed the material’s processing threshold but controlled to avoid over-burning or excessive dross.
4. Conclusion
The diverse process routes of laser cutting technology provide tailored solutions for various materials and quality requirements. From thermochemically driven Flame Cutting to inert-gas-shielded Fusion Cutting and ultra-short-pulse Vaporization Cutting, each process is rooted in specific physical mechanisms. Understanding the interplay between these classifications and parameters is essential for optimizing cutting quality and driving laser manufacturing toward higher precision and efficiency.

Top Stories
Product Categories
- Metal Laser Cutter
- Laser Welder Machine
- Laser Cleaner Machine
- Laser Marker Machine
- Press Brake Machine
Get Easy Solution